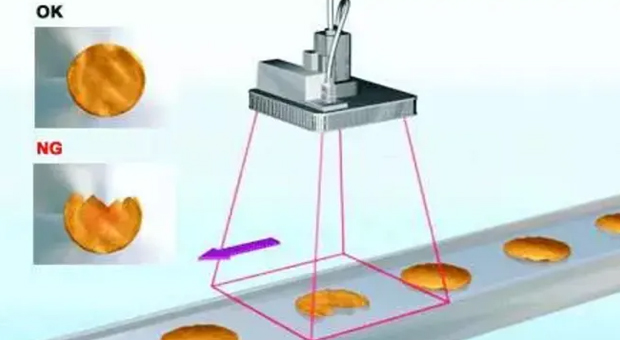
Machine Vision Inspection Application Examples
Machine vision inspection has already established numerous mature and practical applications in industries such as manufacturing, automobiles, 3C electronics, and food and pharmaceuticals. Its core va
2026-09-19
More
In which industries is machine vision inspection applied?
Machine vision inspection, as the core perception technology of intelligent manufacturing, with its advantages of high precision, high speed, and stable operation 24/7, has deeply integrated into the
2026-09-12
More
Applications of Machine Vision in Industrial Inspection
Clear imaging in machine vision is the first step. Due to the reflection and refraction of different material objects' surfaces, as well as other factors, the extraction of the characteristics of the
2026-09-05
More
Introduction to Industrial Cameras and Vision Systems
Industrial cameras are the core imaging hardware of industrial vision systems. Vision systems rely on them to complete image acquisition, analysis, and decision-making as part of an automated inspecti
2026-08-29
More
Industrial Vision Inspection: Definition and Applications Across Industries
Machine vision inspection uses industrial cameras and algorithm systems to simulate human eyes, automatically performing precise detection and classification of object attributes such as size, shape,
2026-08-22
More
Deep Learning Applications in vision Inspection
Deep learning is the core branch of machine vision Inspection. It automatically extracts data features through multiple layers of neural networks and has already achieved large-scale implementation in
2026-08-15
More
Identifying the contour edges of lithium battery tabs applications
With the extreme demands for energy density and safety in batteries, this paper focuses on the profile detection project of lithium battery tabs, a core sub-field of detection. It conducts a horizonta
2026-08-07
More
Machine Vision Technology in Pharmaceutical Defect Inspection
Machine vision is a core intelligent technology for pharmaceutical defect inspection, replacing manual visual checks. Relying on industrial cameras, specialized lighting, and AI algorithms, it can det
2026-07-25
More
What are the advantages of machine vision inspection technology?
A complete machine vision system includes lighting sources, optical lenses, CCD cameras, image acquisition cards, image inspection software, monitors, and communication units.
2026-07-18
More
Multi-Color Switching: High-Performance Fiber Optic Light with Filter Wheel
The fiber optic light(with filter wheel) enables multi-band and multi-color light emission by changing the filter, and can well meet the multi-color detection requirements of different processes and m
2026-07-11
More
 Ms.Cici
 8618319014500